
Vernier Caliper and Micrometer Screw Gauge: Least Count and Zero Error
A vernier caliper has a main scale and a sliding vernier scale. A micrometer has a scale on its sleeve and a second scale on its rotating thimble. First take the reading, then correct it for any zero error, keeping its sign. More digits or a tighter grip do not make a measurement better.
The worked examples below use a vernier resolution of 0.01 cm and micrometer graduations of 0.01 mm. These are example scales, not the scales of every instrument. Check the units and scale on the instrument you are given, and your lesson instructions, before measuring.
Reading a vernier caliper
The outside jaws measure an outside size, such as a ball's diameter. The smaller inside jaws, and the depth probe if there is one, measure other things. Use the faces meant for the task.
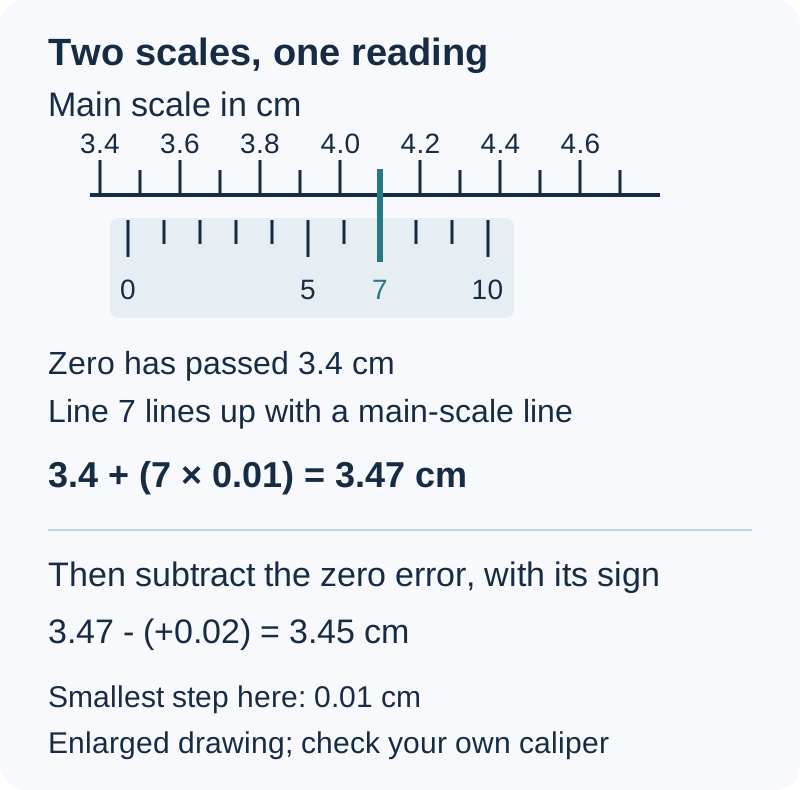
This is an enlarged drawing of a scale, not a photograph of Eclat's instrument. Mitutoyo's caliper explanation describes the sliding-scale principle and gives a different metric resolution example. Always use the resolution of the scale in front of you.
- Read the last main-scale division passed by the vernier zero. Here it is 3.4 cm.
- Find the vernier division that aligns with a main-scale line. Here it is division 7.
- Multiply that division number by the stated resolution: 7 × 0.01 cm = 0.07 cm.
- Add the contributions: 3.4 cm + 0.07 cm = 3.47 cm.
Read from the vernier zero, not the far end of the sliding scale. The zero gives the main reading; the line that matches up gives the small extra part.
Zero error
A zero error means the instrument does not read zero when it should, so every reading it gives is shifted by that amount. For a caliper whose scale starts at zero, close the jaws gently, as you were shown, and check the reading. A positive zero error means it reads above zero with the jaws closed; a negative error means it reads below zero. With a negative vernier error, the aligned division alone is not its signed value. Follow the scale's negative-reading convention.
Because the error is already inside every reading, the correction is always measured reading minus signed zero error. Keep the unit the same throughout.
| Measured reading | Signed zero error | Corrected reading |
| 3.47 cm | +0.02 cm | 3.47 - (+0.02) = 3.45 cm |
| 2.36 cm | +0.02 cm | 2.36 - (+0.02) = 2.34 cm |
| 2.36 cm | -0.02 cm | 2.36 - (-0.02) = 2.38 cm |
These are made-up readings. The second and third rows show why the sign matters when you work out a ball bearing's diameter. Apply the error once to the whole reading, not once to each part of it. If zero checks before and after measuring disagree, report the change rather than choosing the more convenient value.
Reading a micrometer screw gauge
The anvil is the fixed measuring face; the spindle is the moving face. The sleeve, also called the barrel, carries the main scale and the datum line you read against. The rotating thimble adds the hundredths of a millimetre. A ratchet, friction thimble or similar part limits how hard the faces press on the object.
For the 0.01 mm example scale:
- Read the whole millimetres visible on the sleeve.
- Check whether the next half-millimetre mark is also visible.
- Read the thimble division at the sleeve's datum line.
- Add its contribution, then correct for signed zero error.
Mitutoyo's illustrated scale guide distinguishes standard, vernier and mechanical-digit micrometers. The guide shows different reading increments. Check your instrument's scale before applying this example.
Worked reading and ball-bearing example
| Step | Example sleeve/thimble reading | Separate ball-bearing example |
| Whole and half millimetres visible | 5.50 mm | 4.50 mm |
| Aligned thimble division | 23 | 18 |
| Thimble contribution at 0.01 mm per division | 0.23 mm | 0.18 mm |
| Measured reading | 5.73 mm | 4.68 mm |
| Signed zero error | 0.00 mm | -0.03 mm |
| Corrected reading | 5.73 mm | 4.68 - (-0.03) = 4.71 mm |
Missing the half-millimetre mark changes the first result by 0.50 mm, because one full turn of a standard metric thimble moves the spindle only 0.5 mm (Wikipedia: micrometer). Check that mark before adding the thimble reading. For zero checks, use the reference you are given and the ratchet or friction thimble on your micrometer, as you were shown. If its range does not start at zero, use the reference you are given. Do not try to close it beyond its range.
Why grip force matters
Mitutoyo's ratchet-thimble example uses a preset measuring force. Other models work differently, so ask your trainer to show you yours. A click does not mean you should keep tightening.
A soft object can be squashed by the faces, so a reading taken with too much force measures the squashed size. Repeated readings at the same force can agree and still all be too small. Open the faces before you move the object. Stop if the movement sticks, something is damaged or the readings are inconsistent, instead of forcing the instrument.
Digital calipers
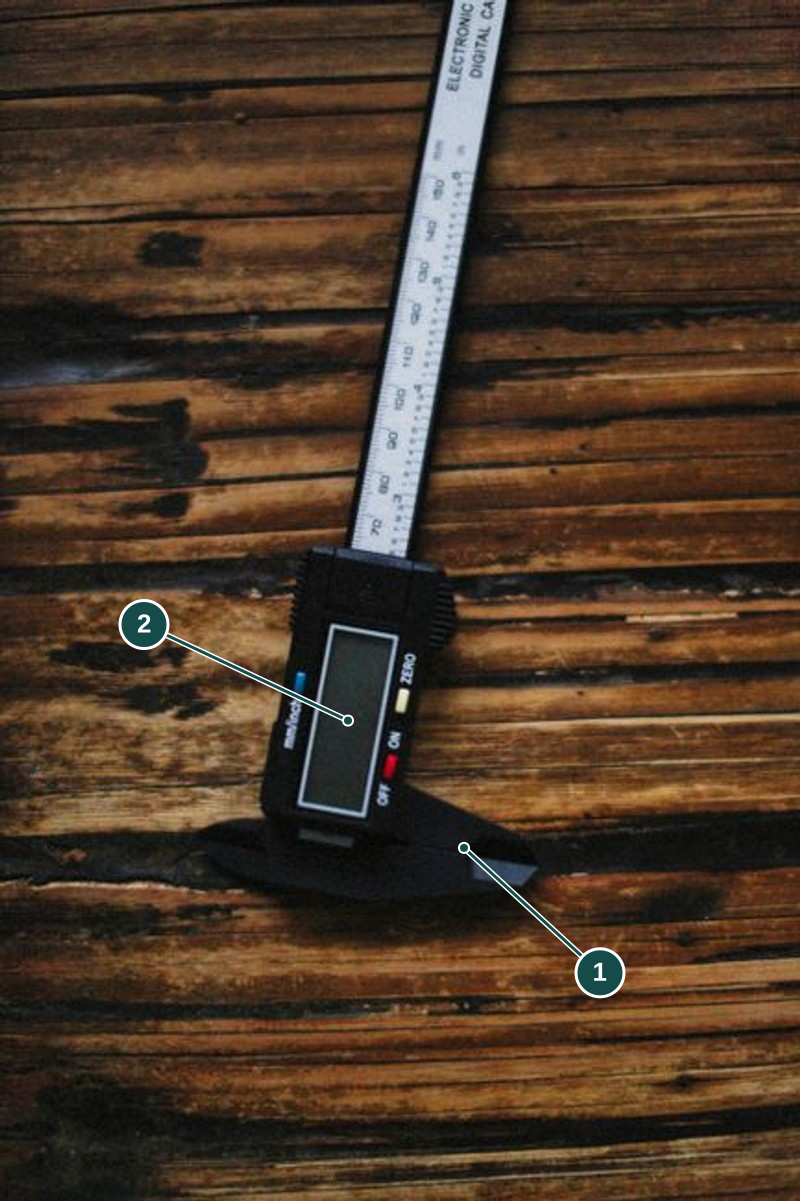
- Outside jaws. Close them on the outside of the object, lined up as you were shown and with light force.
- Display. Shows the reading; check the units and the zero setting for your model.
Illustrative photo: Alexey Demidov on Pexels.
A digital display saves you the vernier sum, but the jaws still have to touch the object properly and squarely. The smallest step on the display does not tell you how accurate it is. Mitutoyo's caliper guidance discusses light measuring force and how zeroing differs between models, so do not assume every model resets the same way.
What a zero check does not tell you
A zero check tests one point, not every reading across the scale. Two instruments can agree at zero and still disagree when measuring an object. Do not decide which is right from the number of digits or the type of instrument.
Mitutoyo's handling guide identifies several influences on caliper readings, including contact force, jaw alignment, viewing angle and temperature differences. These are things to check, not a way to diagnose one mismatch. Your teacher chooses how to compare the instruments.
Before you explain a disagreement, make sure the object, the measuring faces and the contact point were the same. If a reading changes when you tighten, tilt or move the jaws, report it. Do not keep adjusting until the instrument displays the expected value.
When readings differ along an object
Suppose a wire gives different diameter readings at two places. The wire may really be thicker in one place, the contact may have changed, or something else went wrong. The two numbers alone do not tell you which. Record where and how each reading was taken, then repeat as your method says.
Repeating at one place tells you how consistent your reading is; measuring along the wire tells you whether the wire varies. Do not simply average the two kinds together. The wire resistance practical controls which dimensions and locations are needed for its calculation.
For a ball bearing, first check that you are measuring its outside diameter with the right faces. Measuring across a different diameter or direction, at a slant, or touching a different part changes what you measure. Readings that agree are useful, but they do not prove the ball's exact size or shape.
Choosing the instrument and recording
Choose an instrument that suits the size you are measuring, the object, how precise the result must be and the method you are allowed to use. The table compares the example scales used here; it is not a rule for every instrument.
| Example instrument | Example scale increment | Relevant measurement |
| Millimetre ruler | 1 mm | Length between two positions |
| This vernier scale | 0.1 mm, equal to 0.01 cm | Outside or inside size, or depth, using the right faces |
| This micrometer scale | 0.01 mm | Small outside size within the micrometer's range |
Record the unit, and as many decimal places as your instrument reads to and your lesson asks for. For these examples, 3.40 cm and 5.00 mm keep the last measured place, even when it is zero. Keep the reading, the zero error and the corrected result separate so someone can check your working.
Before measuring a fragile, sharp or unfamiliar object, check with your trainer that it is suitable. Keep fingers clear of closing faces. Measuring jaws are not clamps, levers or tools for pulling an object. Use the lab safety briefing principles before starting.
What teachers and technicians check
Staff match the instrument's range, faces and force-limiting part (a ratchet or friction thimble) to the object and the measurement. They show you the zero check and how to use that part, inspect the instrument and decide whether one that gives inconsistent readings needs checking or replacing. There is no standard number of clicks or reset routine that carries over from another model.
You record the instrument, units, where you measured, the raw reading and the signed correction. Report stiff movement, sharp or damaged faces and any change in the zero check. Repairs, cleaning products and adjustments are for staff. Correcting for zero error does not fix a reading taken on the wrong part of the object, or with the faces tilted or pressed too hard.
For practice, pair this guide with the wire resistance experiment, meniscus and parallax guide and sources of error guide. The O-Level Physics practical hub and practical overview cover the wider course. For supervised coaching, see O-Level Physics tuition.
Sources
- https://www2.mitutoyo.co.jp/eng/useful/E11003/pageindices/index23.html
- https://www.mitutoyo.com/metrology-insights/mitutoyo-calipers-digital-dial-and-vernier-calipers-precision-measurement-tools-for-manufacturing/
- https://isomer-user-content.by.gov.sg/334/42ee79d0-bb13-43f5-94ab-629729f88aa0/6091_y26_sy.pdf
- https://en.wikipedia.org/wiki/Micrometer_(device)
Save or continue learning
Want supervised lab practice?
Explore practical lessons, with timings, fees, and locations on the programme page.
View O-Level Physics Practicals (Labs & Experiments)